McLanahan Drag & Reclaim Feeders
McLanahan Drag & Reclaim Feeders
Reliable Material Reclaiming and Controlled Feeding
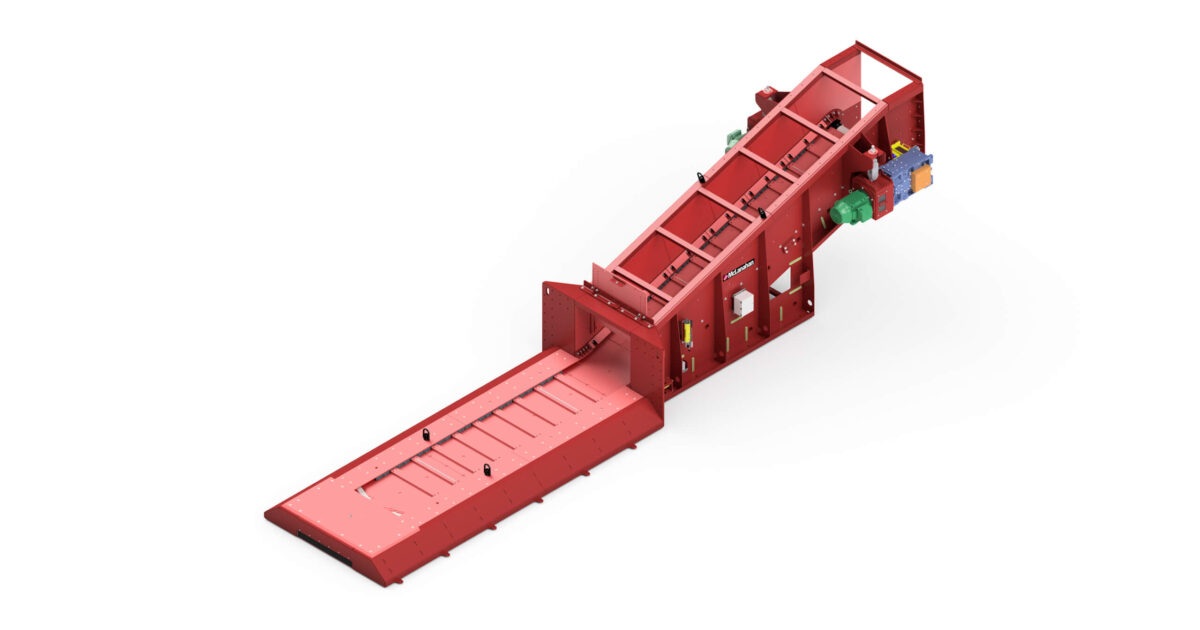
McLanahan Drag & Reclaim Feeders are heavy-duty material handling and feeding systems designed to reclaim stored material from stockpiles, bins, hoppers and surge piles while providing a controlled and consistent feed to downstream equipment.
They are designed for applications where material needs to be efficiently withdrawn from storage and delivered at a controlled rate to conveyors, crushers, screens or other processing equipment.
Drag & Reclaim Feeders provide an effective solution for combining material reclaiming and controlled feeding in a single system.
How McLanahan Drag & Reclaim Feeders Work
Material is stored above or around the reclaiming area, typically within a stockpile, hopper, bin or surge pile.
A series of heavy-duty flights or paddles connected to chains moves along the bottom of the storage area.
As the chain and flight assembly travels, the flights drag material toward the discharge point.
The feeder continuously withdraws material from the storage area and delivers it to the downstream conveyor or processing equipment.
The speed of the drag chain can be controlled to regulate the amount of material being reclaimed.
Controlled Reclaiming
One of the primary functions of a Drag & Reclaim Feeder is to provide controlled withdrawal of material from a storage area.
Instead of allowing material to flow freely from the stockpile or hopper, the feeder controls the rate at which material is removed.
This provides a more consistent feed to downstream equipment and can help prevent surges and uncontrolled material flow.
Stockpile Reclaim
Drag & Reclaim Feeders are particularly useful for reclaiming material from stockpiles and surge piles.
They can be installed beneath stored material to continuously withdraw and transfer material without requiring conventional front-end loading equipment for every reclaiming operation.
This can reduce material handling requirements and improve the efficiency of the overall material handling system.
Heavy-Duty Material Handling
The feeder is designed to operate under the weight and pressure of stored material.
Heavy-duty chains, flights, drive components and structural elements are selected according to the application requirements.
This allows the system to handle large quantities of material and operate under demanding mining and mineral processing conditions.
Consistent Feed to Downstream Equipment
A controlled reclaiming rate allows the Drag & Reclaim Feeder to provide a more consistent feed to downstream equipment such as:
-
Crushers
-
Screens
-
Conveyors
-
Mills
-
Processing plants
-
Other material handling equipment
A consistent feed can help improve process stability and reduce fluctuations throughout the processing circuit.
Applications
McLanahan Drag & Reclaim Feeders are suitable for applications including:
-
Mining
-
Mineral processing
-
Aggregate processing
-
Stockpile reclaim
-
Surge pile reclaim
-
Hopper discharge
-
Bin discharge
-
Material transfer
-
Crusher feeding
-
Conveyor feeding
-
Bulk material handling
Typical materials include:
-
Coal
-
Limestone
-
Iron ore
-
Copper ore
-
Gold ore
-
Phosphate rock
-
Aggregates
-
Sand
-
Gravel
-
Other bulk materials
Application suitability depends on material characteristics, storage conditions, capacity requirements and feeder configuration.
Key Features & Benefits
-
Controlled material reclaiming
-
Combines reclaiming and feeding
-
Suitable for stockpiles, bins, hoppers and surge piles
-
Continuous material withdrawal
-
Adjustable feed rate
-
Heavy-duty chain and flight construction
-
Suitable for large quantities of stored material
-
Robust drive system
-
Suitable for demanding mining applications
-
Provides consistent feed to downstream equipment
-
Can reduce manual or mobile equipment reclaiming requirements
-
Can be integrated with conveyors and crushing circuits
-
Designed for reliable continuous operation
Factors Affecting Drag & Reclaim Feeder Performance
Actual capacity and performance depend on several factors, including:
-
Material type
-
Bulk density
-
Material moisture
-
Material hardness
-
Material abrasiveness
-
Particle size
-
Storage pile height
-
Material pressure on the feeder
-
Feeder width
-
Feeder length
-
Chain speed
-
Flight configuration
-
Hopper or stockpile geometry
-
Required feed rate
-
Installed power
Proper feeder and storage-area design are important for achieving consistent reclaiming and controlled material flow.
Selecting the Right Drag & Reclaim Feeder
The appropriate feeder should be selected based on:
-
Material type
-
Required capacity (TPH)
-
Bulk density
-
Maximum particle size
-
Material hardness
-
Abrasiveness
-
Moisture content
-
Storage volume
-
Stockpile or hopper geometry
-
Required reclaim rate
-
Feeder width and length
-
Downstream equipment
-
Installation arrangement
-
Operating conditions
Cube Solutions can evaluate your application requirements and assist in selecting the appropriate McLanahan Drag & Reclaim Feeder configuration.
McLanahan Drag & Reclaim Feeders from Cube Solutions
As a McLanahan agent, Cube Solutions provides feeding, reclaiming, crushing and mineral processing solutions for customers in Egypt and the region.
Our services include equipment selection, application evaluation, technical support and supply of McLanahan equipment.
Contact Cube Solutions to discuss your Drag & Reclaim Feeder application and determine the most suitable configuration for your operation.